 Impact Wrench
 Screwdriver
 Cordless Drill
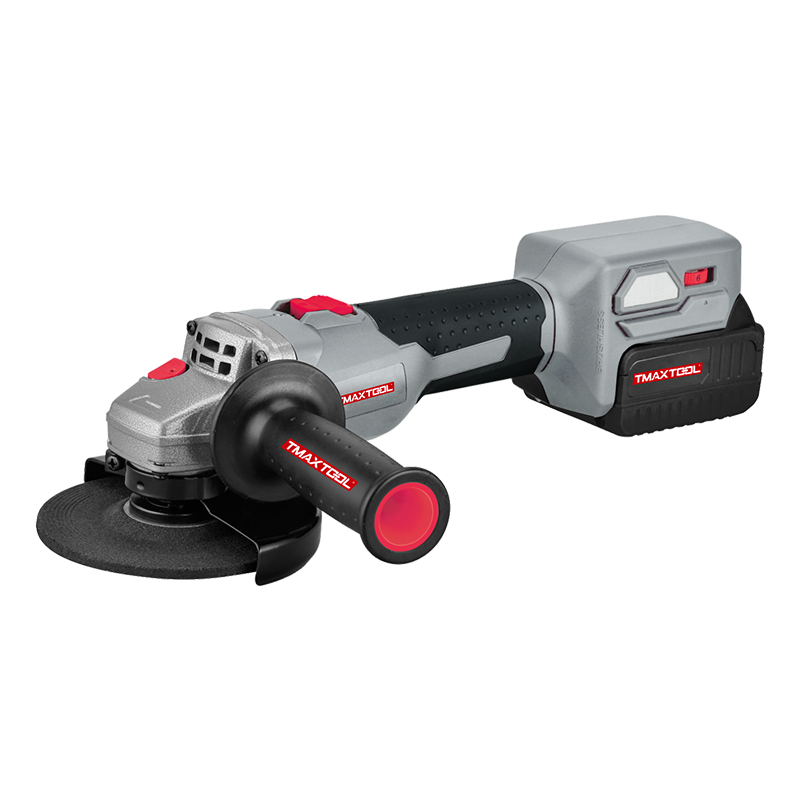 Angle Grinder
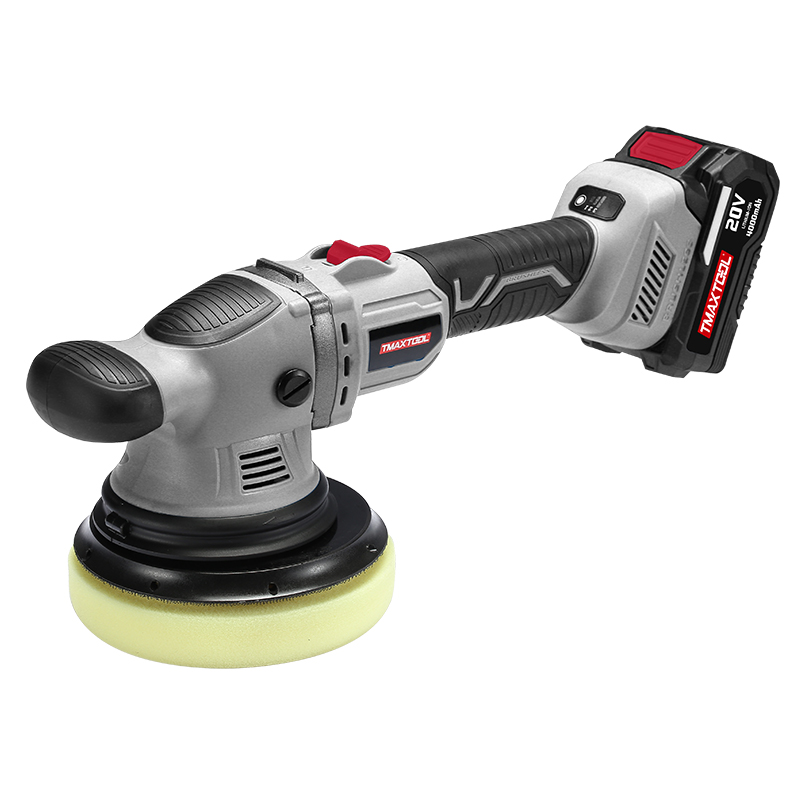 Polisher
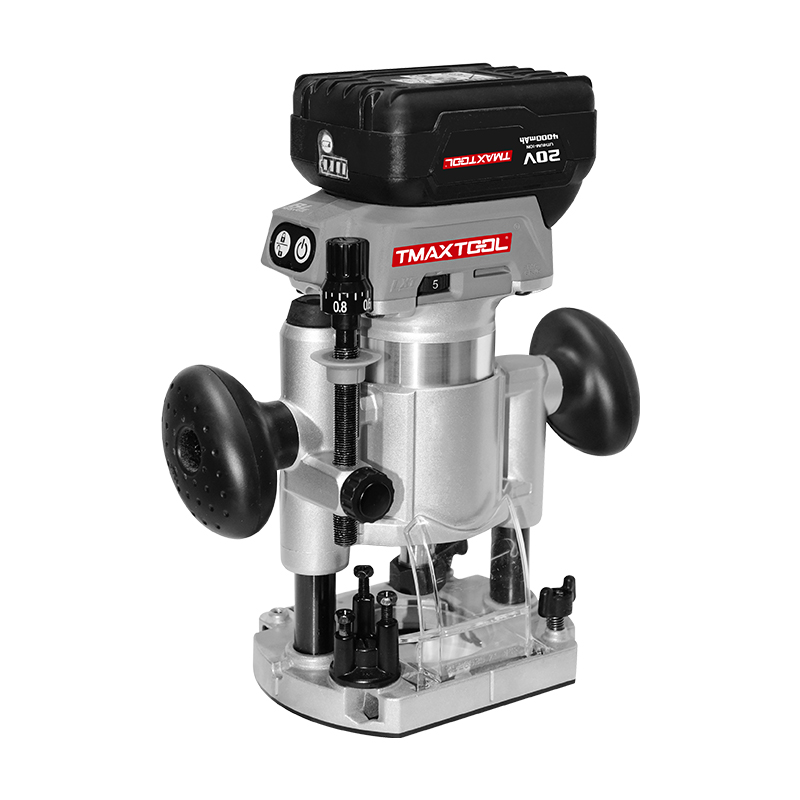 Wood Router
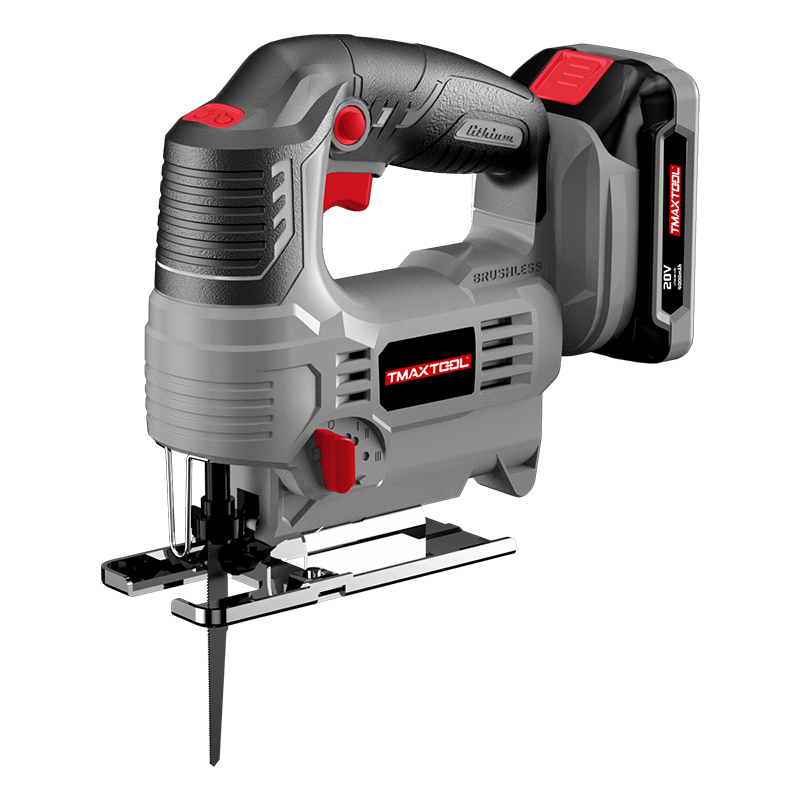 Jig Saw
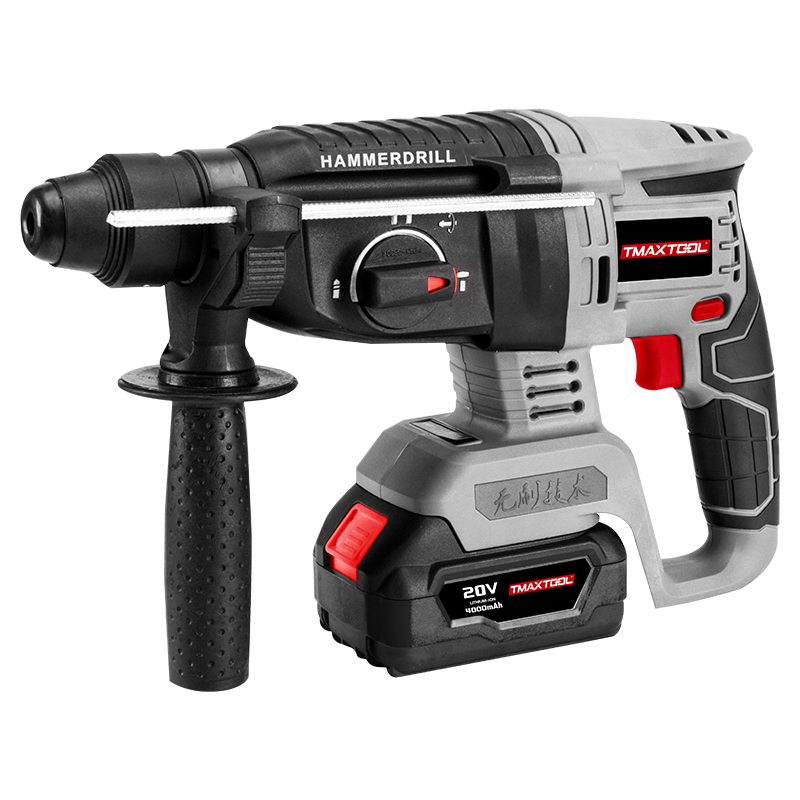 Hammer Drill
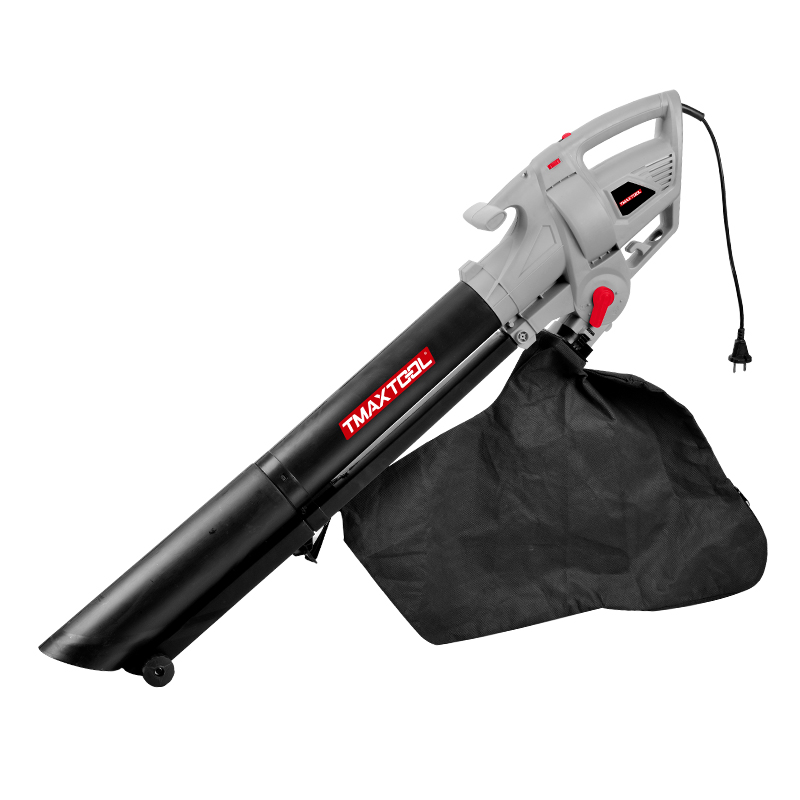 Portable Blower
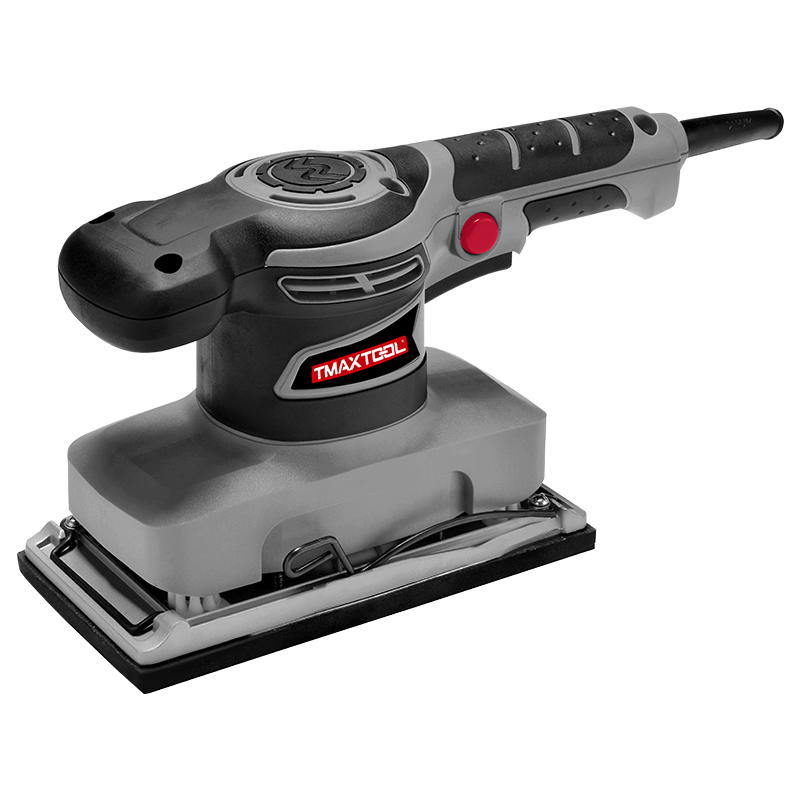 Orbital Sander
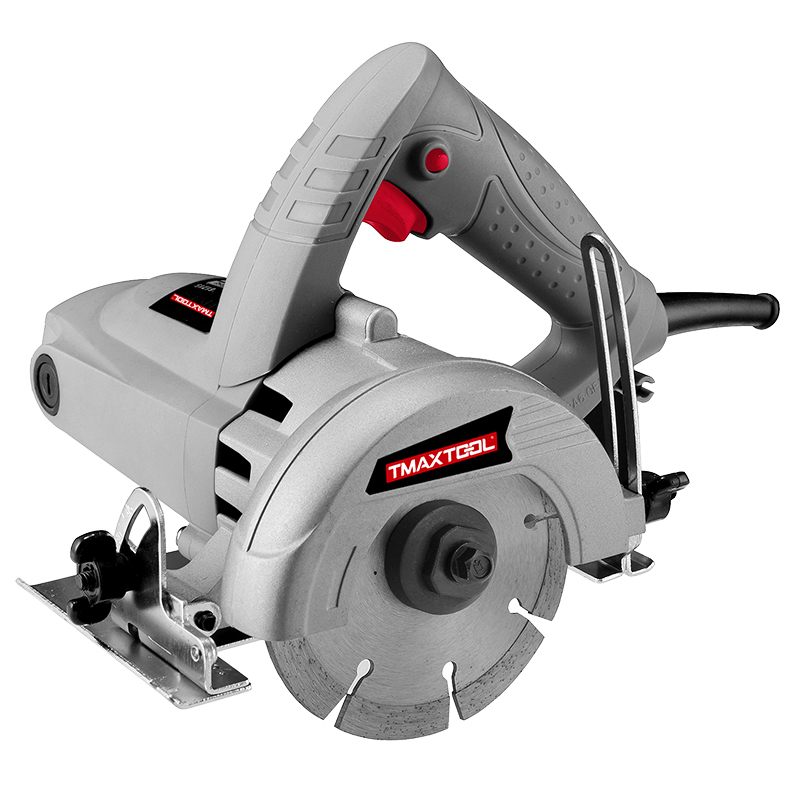 Marble Cutter
 GARDEN TOOLS
 Battery Chain Saw
 Battery Brush Cutter
 Battery Hedge Trimmer
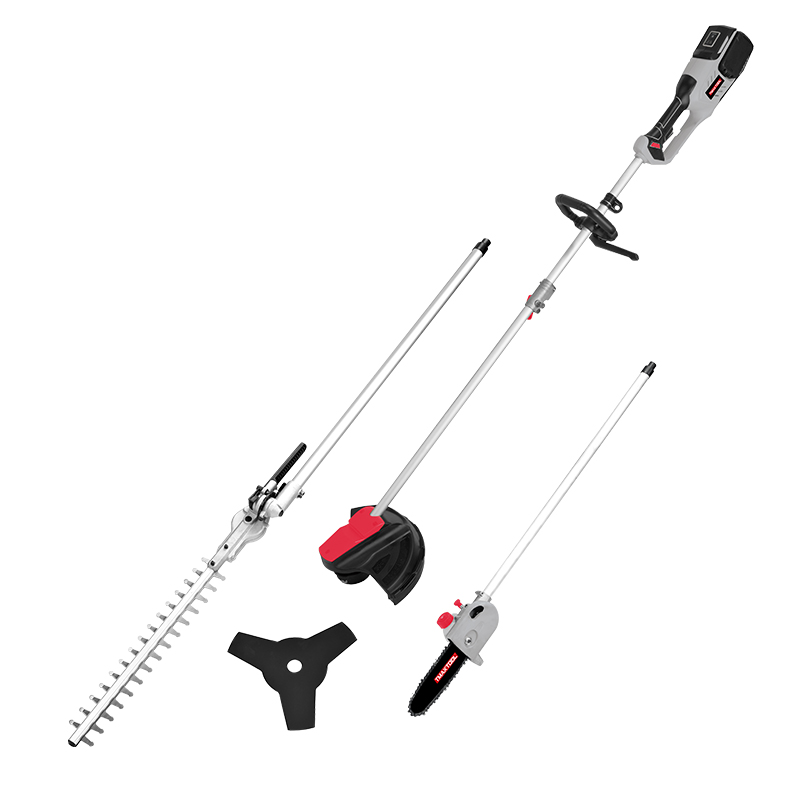 Battery Multi Tool
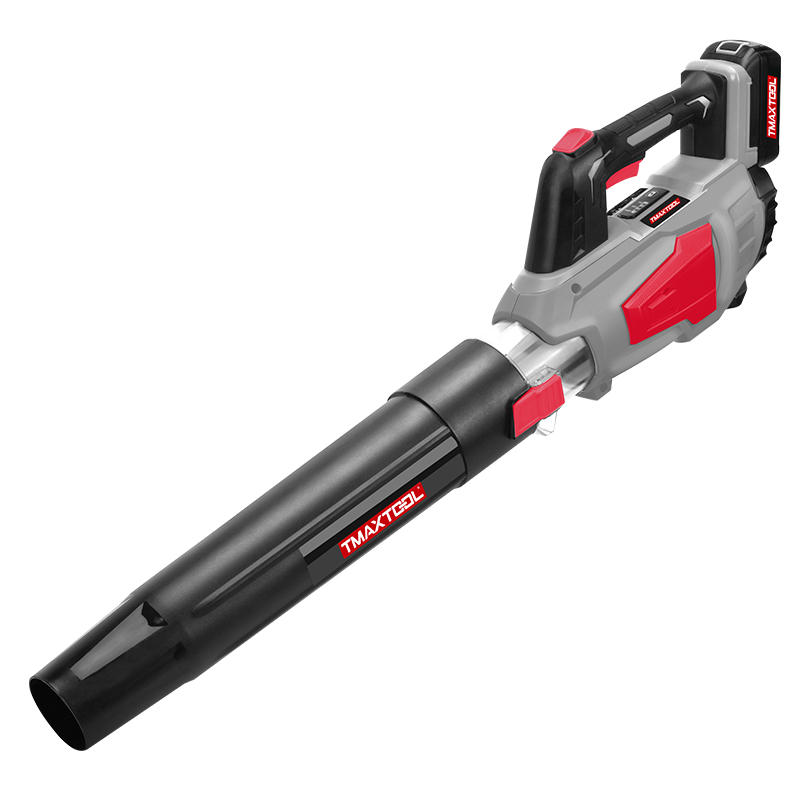 Battery Blower
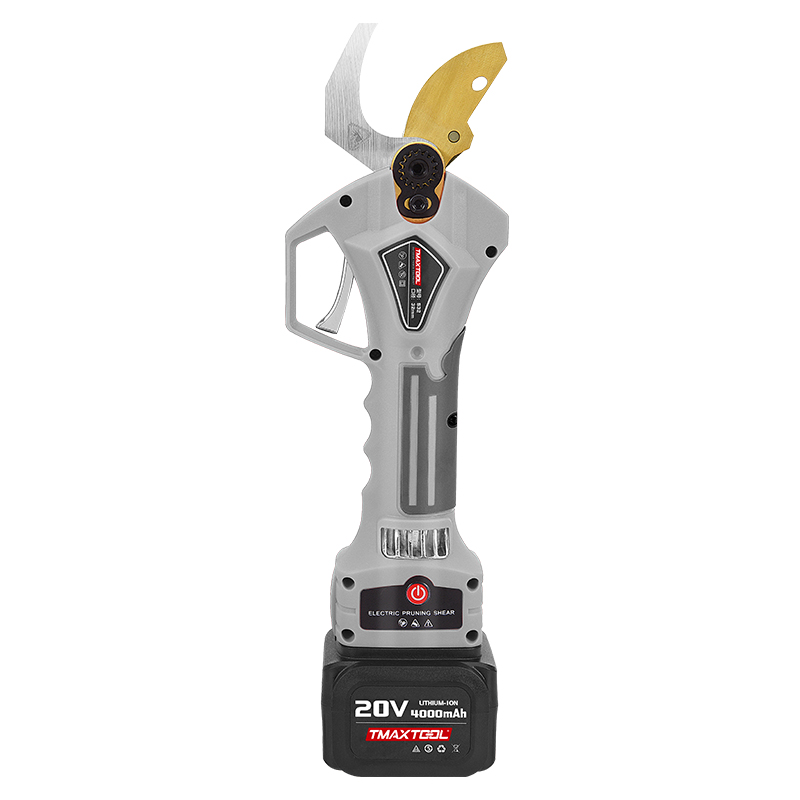 Batter Pruning Shears
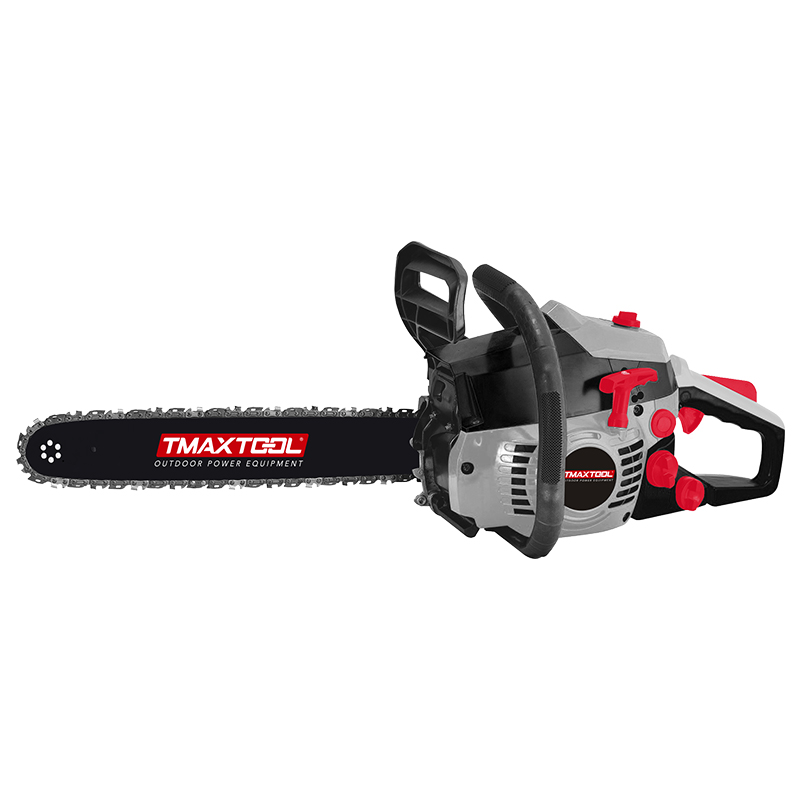 Chain Saw
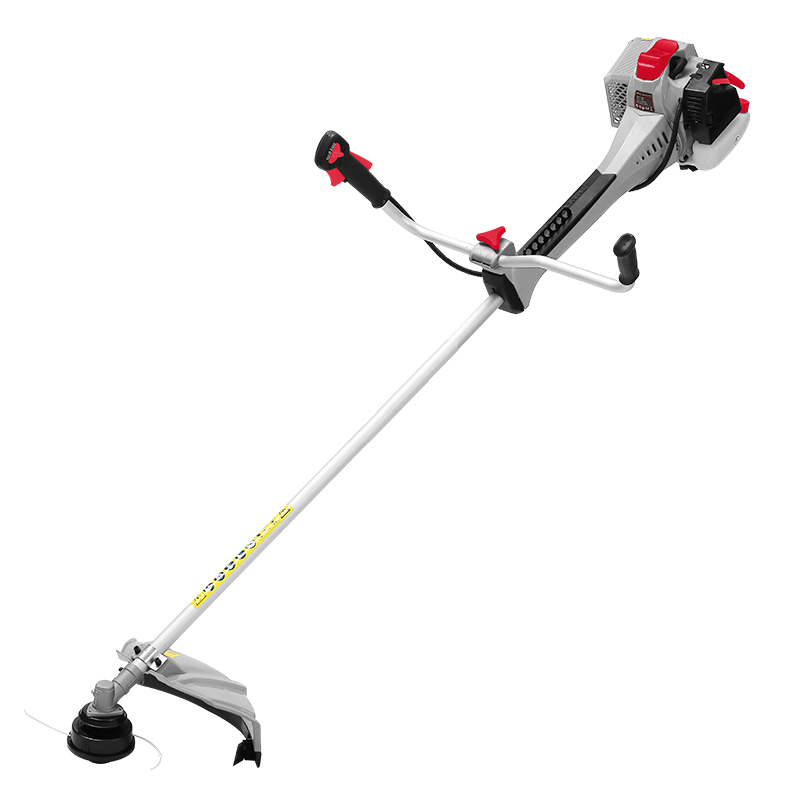 Brush Cutter
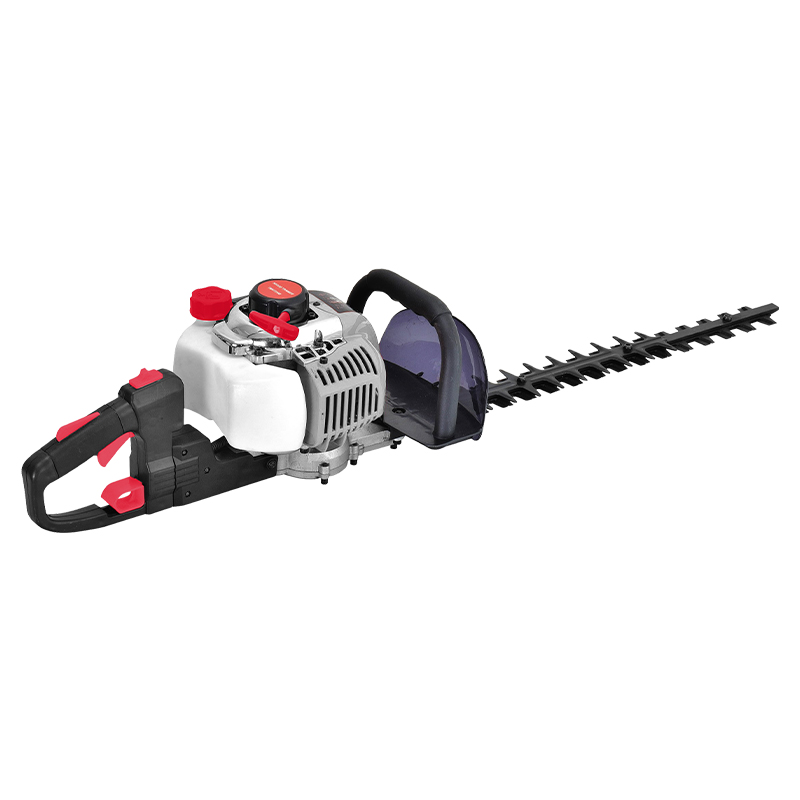 Hedge Trimmer
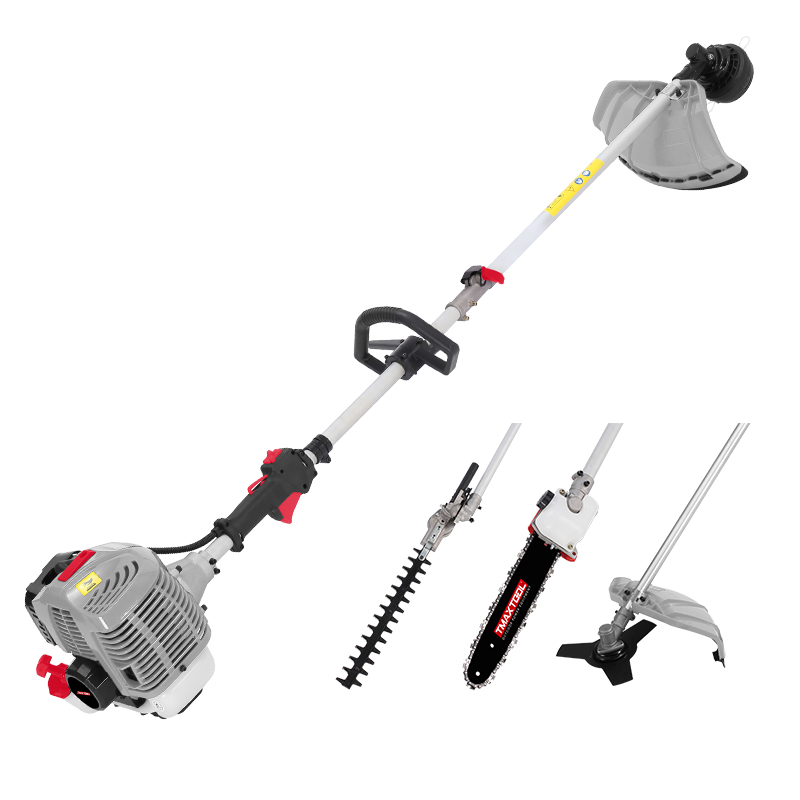 Multi Tool
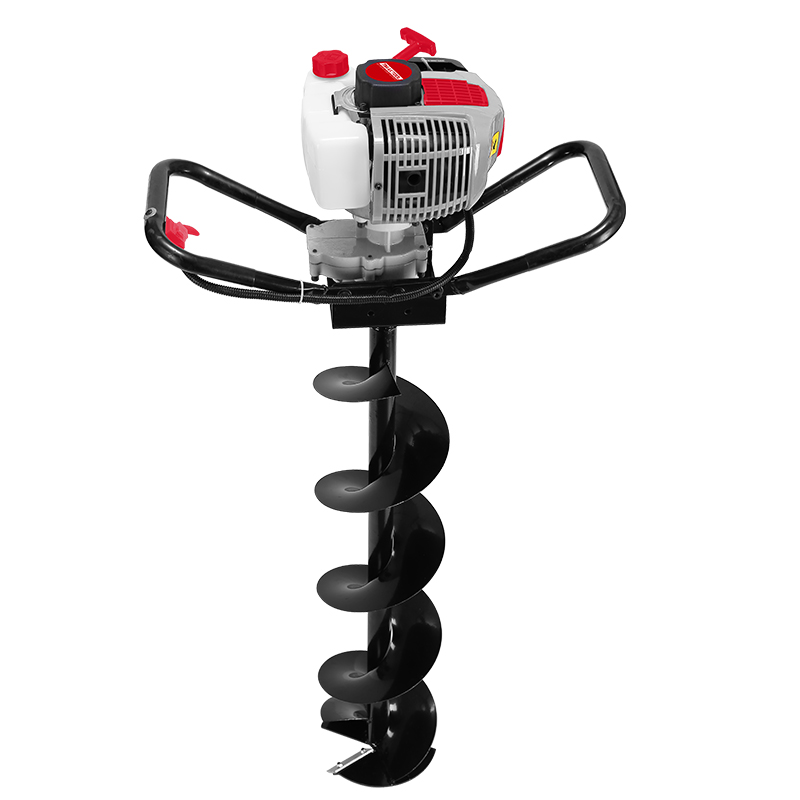 Earth Auger
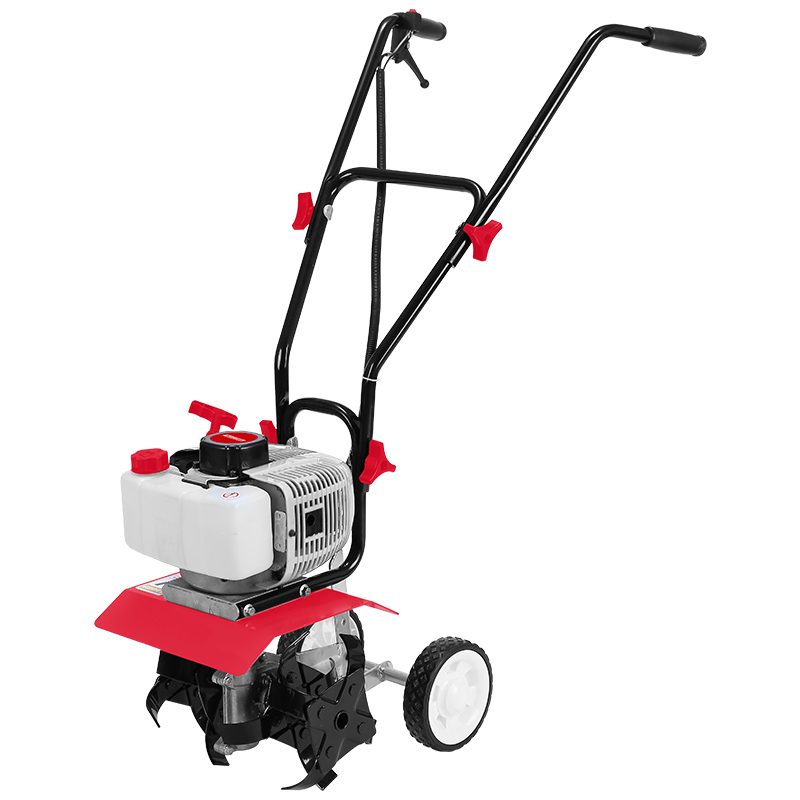 Tiller
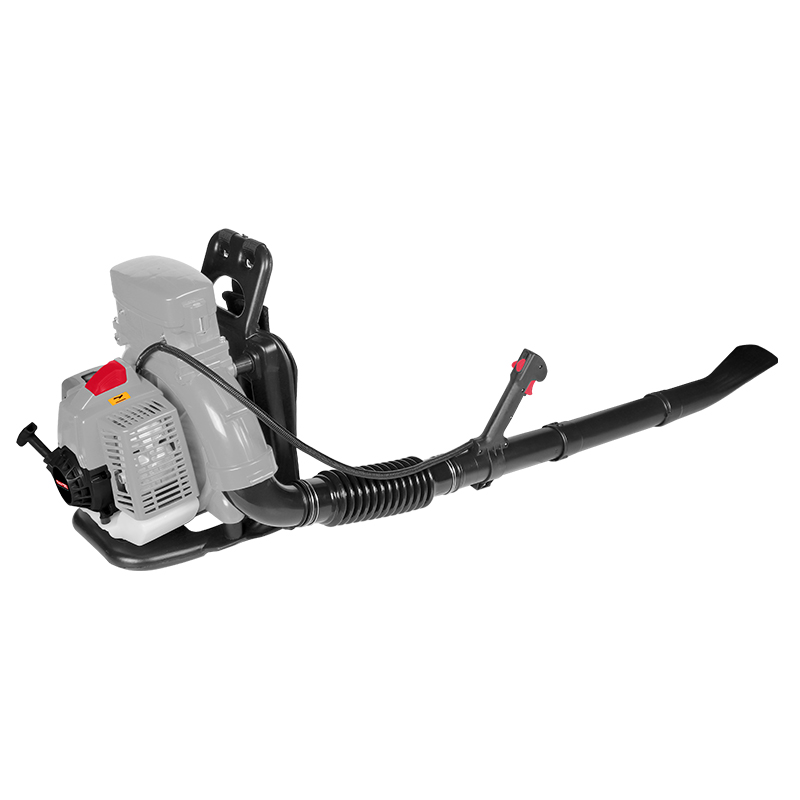 Blower
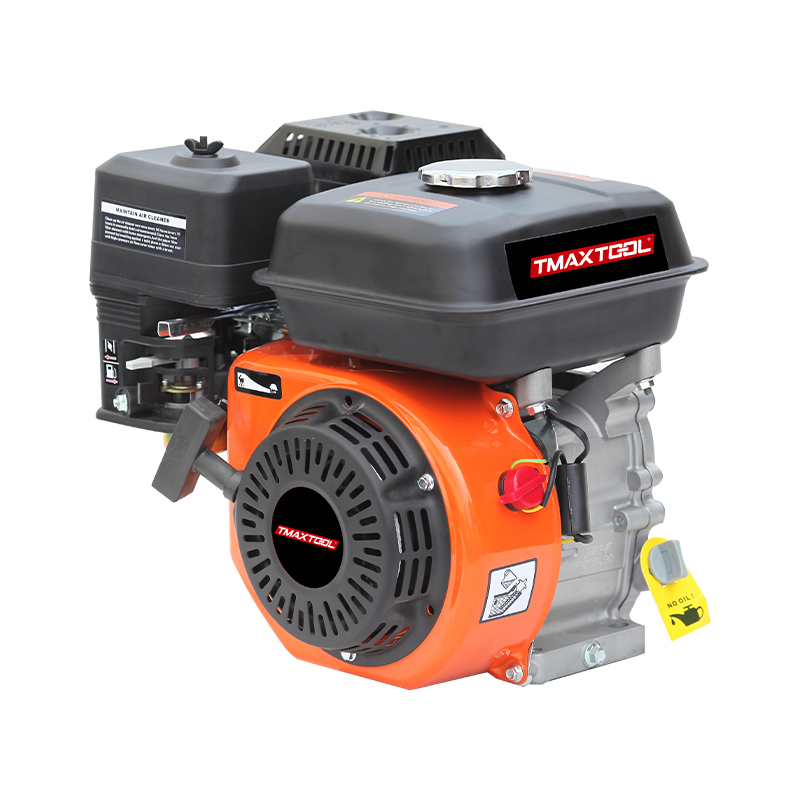 4 Stroke Gasoline Engine
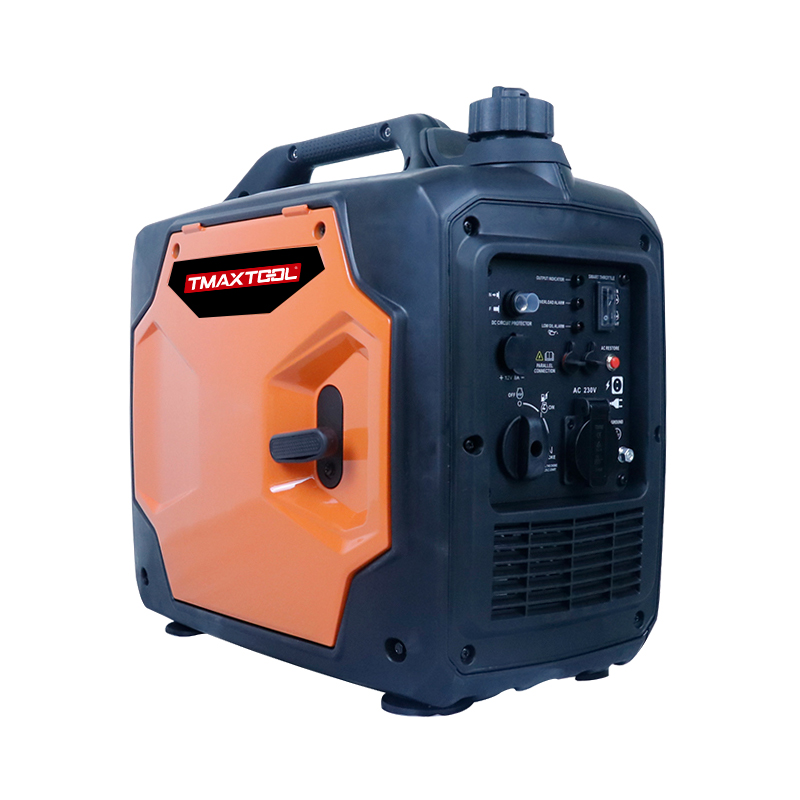 Generator
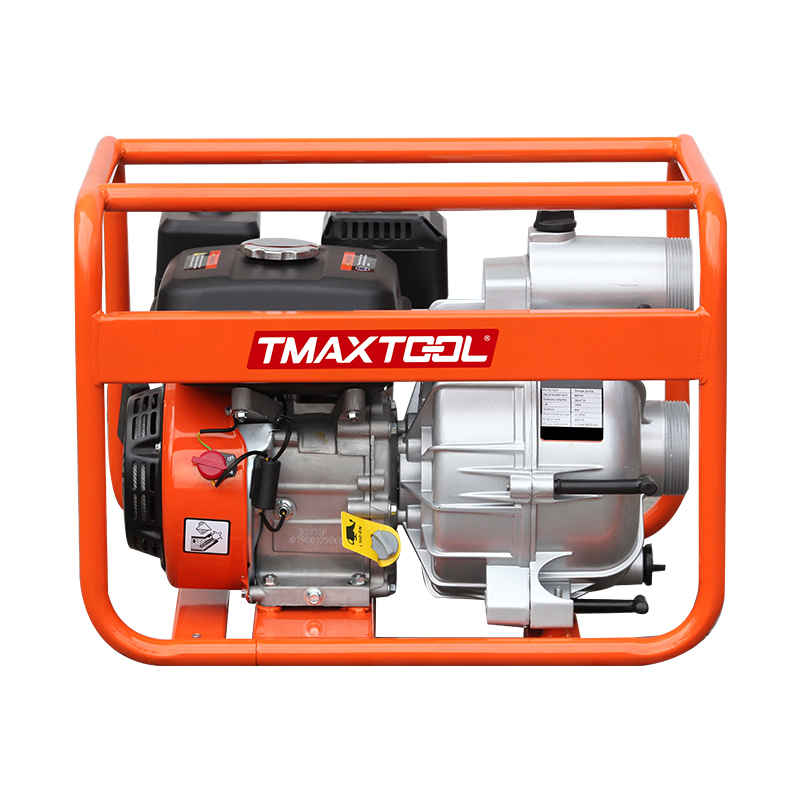 Water Pump
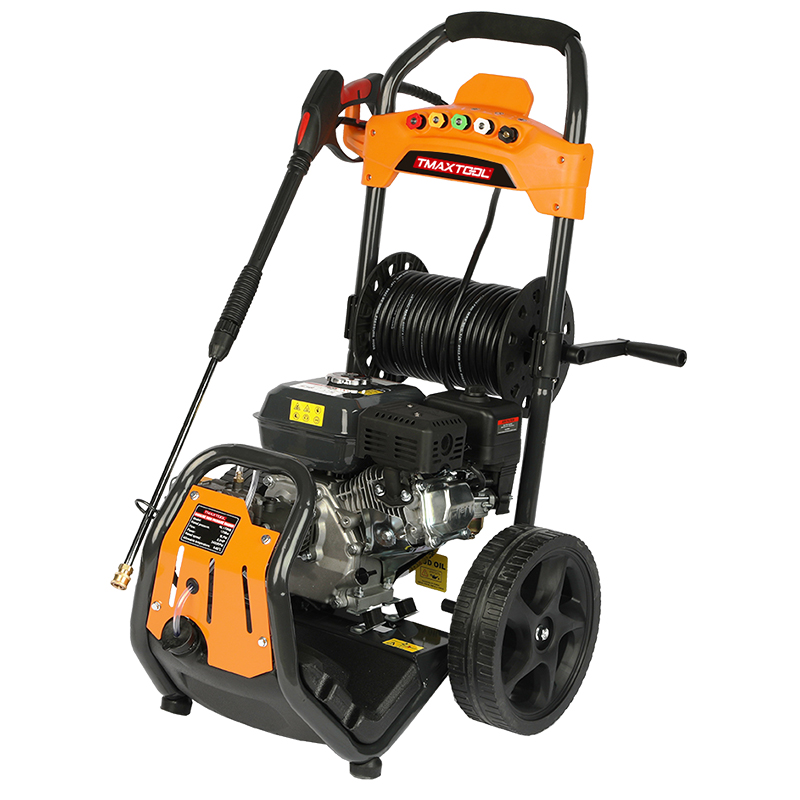 High Pressure Washer
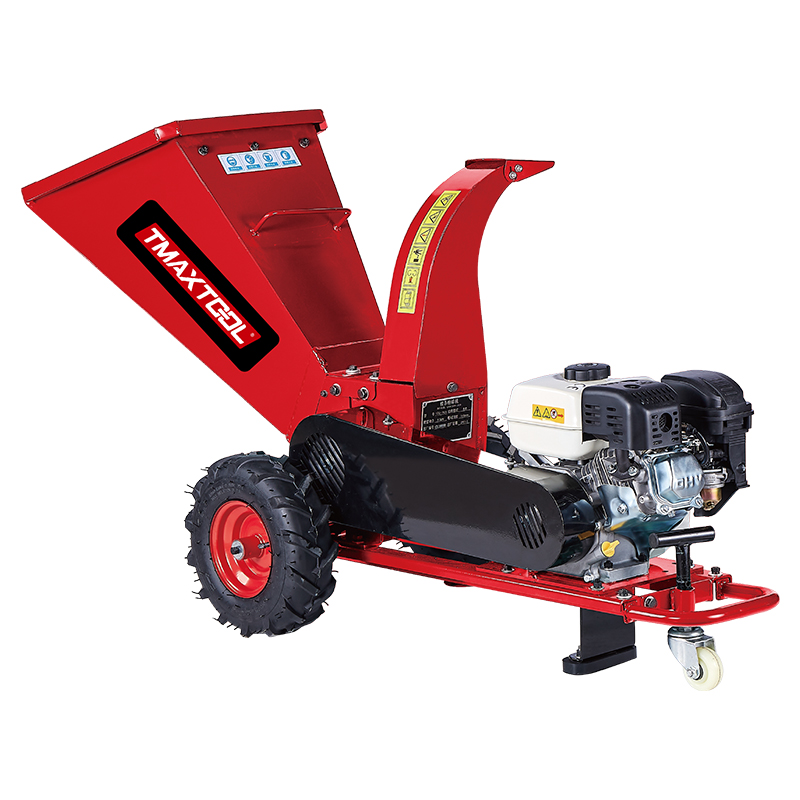 Wood Cutter
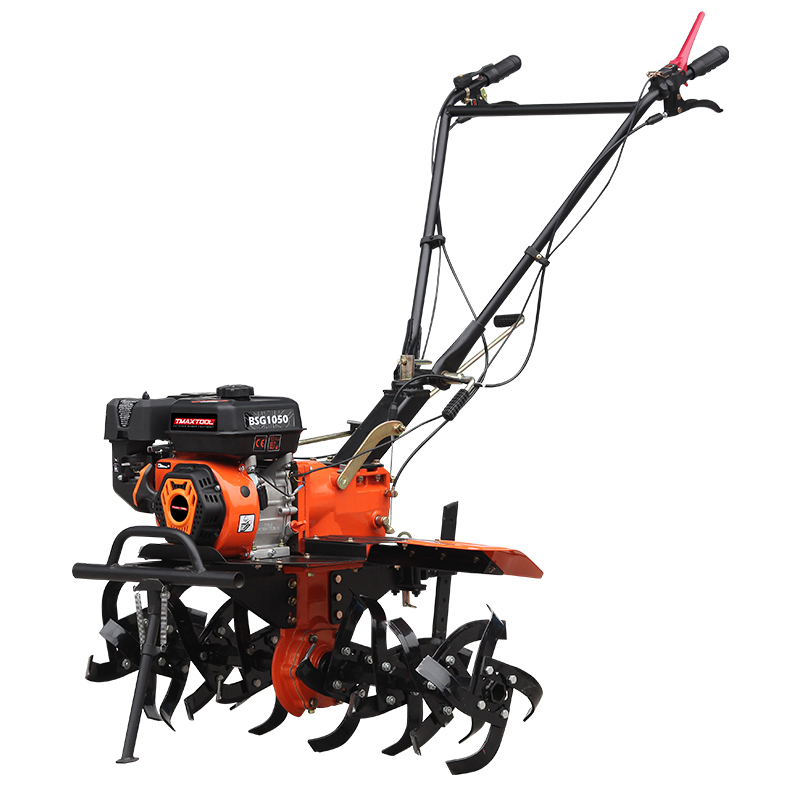 4 Stroke Tiller
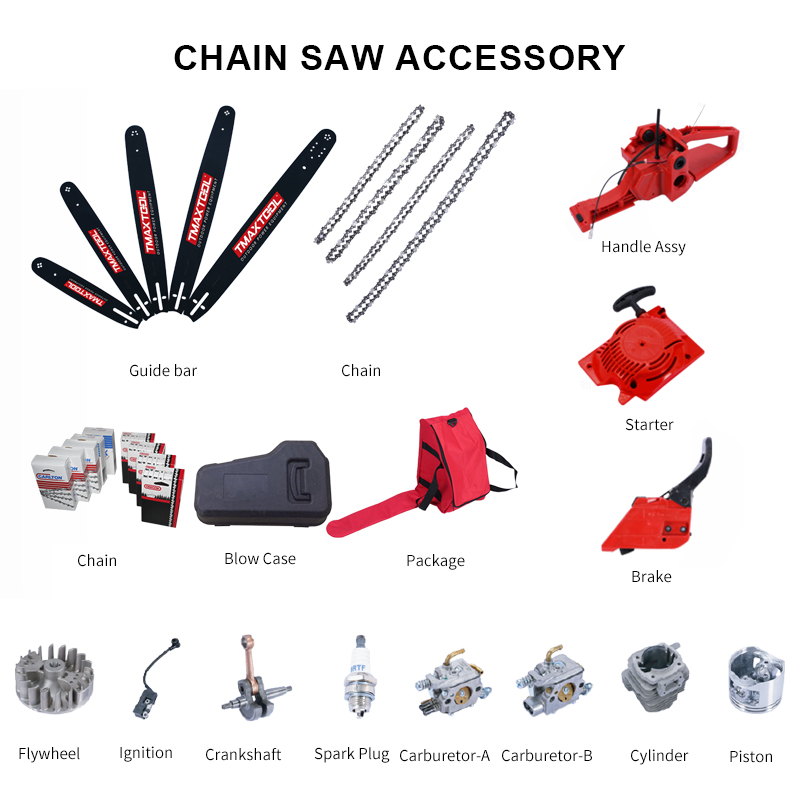 Chain Saw Accessory
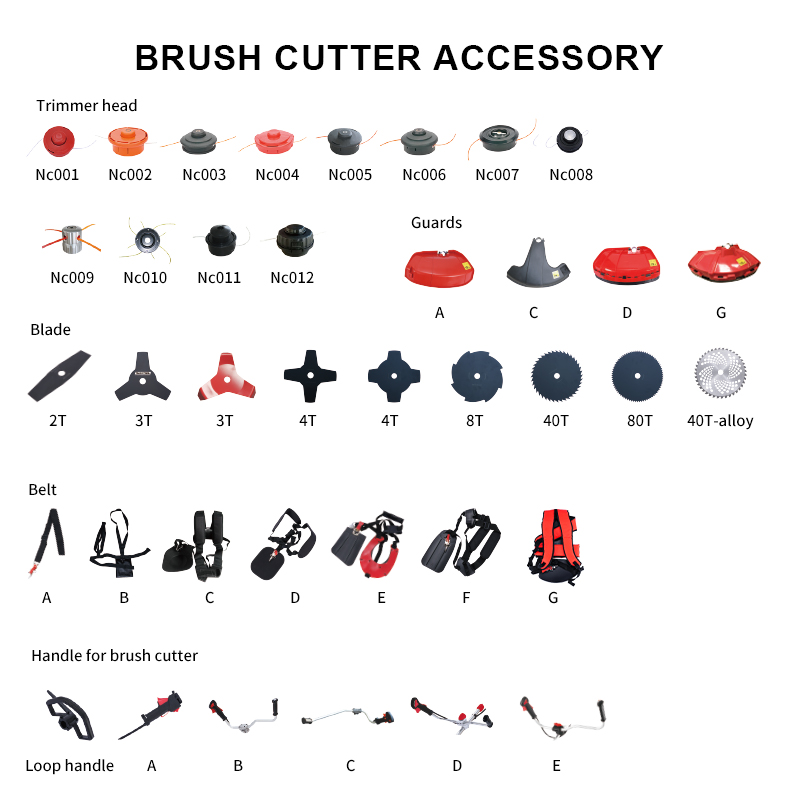 Brush Cutter Accessory
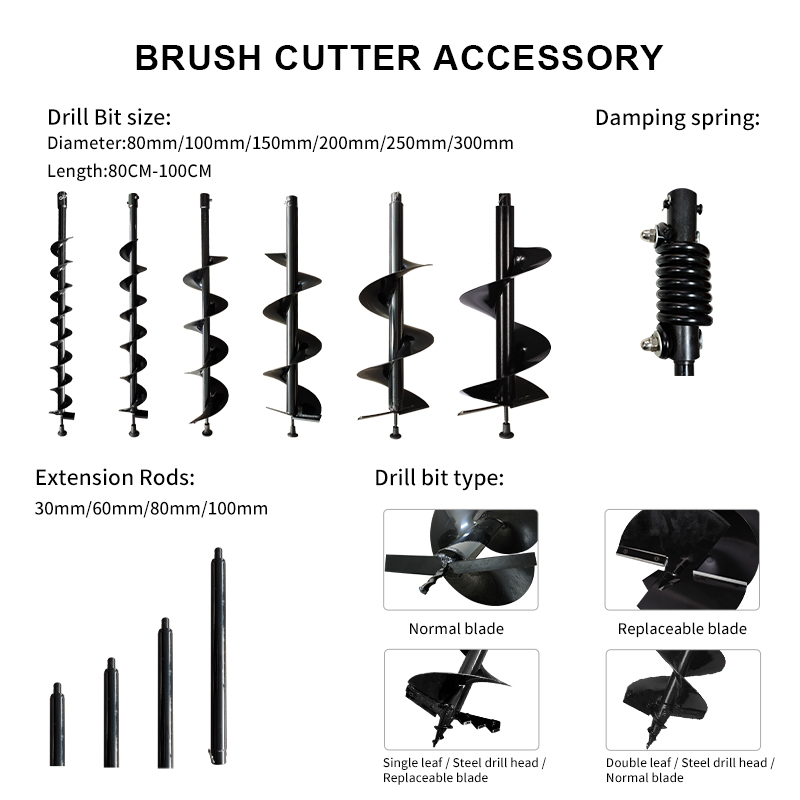 Earth Auger Accessory
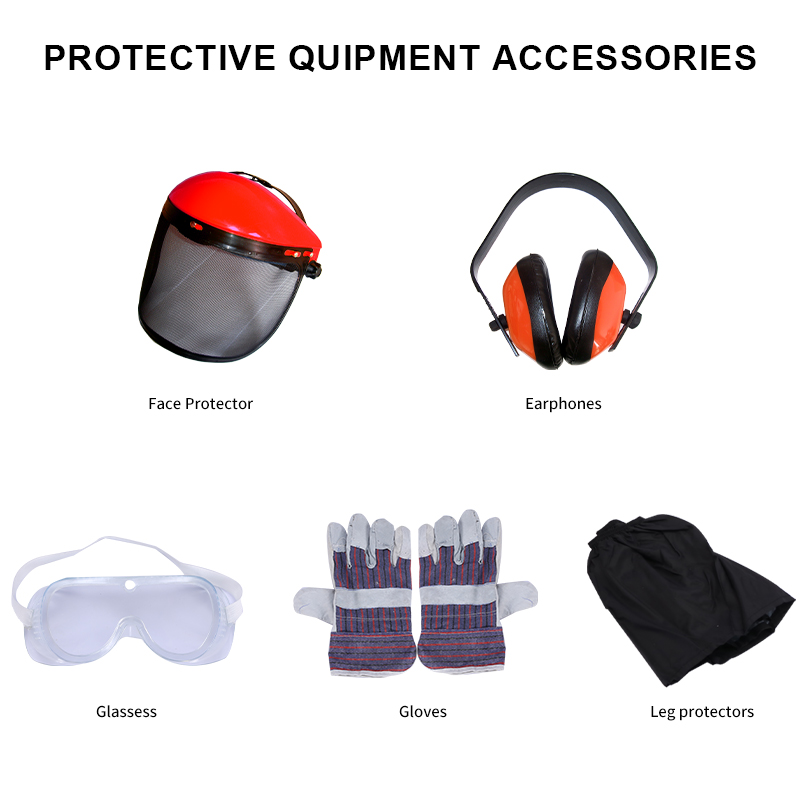 Protective Equipment Accessories
Leave Your Message


Agricultural Machinery Quality Inspection Guide
Agricultural Machinery Quality Inspection Guide: A Complete Handbook for Global Buyers
Table of Contents
- Understanding Why Rigorous Quality Inspection Matters for Farm Equipment
- Core Pre-Inspection Preparation & Document Verification
- Step 1: Visual & Structural Full Machine Inspection
- Step 2: Critical Power & Engine System Functional Testing
- Step 3: Hydraulic, Transmission & Moving Assembly Inspection
- Step 4: Safety Component & Compliance Standard Check
- Step 5: Category-Specific Inspection Checklists
- Handheld Garden & Forestry Tools
- Rotary Tillers, Cultivators & Soil Preparation Equipment
- Sprayers, Water Pumps & Irrigation Machinery
- Generators & Portable Power Units
- Step 6: Component & Accessory Quality Validation
- Step 7: Packaging & Shipment Condition Inspection
- Defect Classification & Shipment Decision Rules
- International Compliance Certifications Buyers Must Verify
- Advanced Lab & Field Performance Testing Techniques
- Frequently Asked Questions About Agri Machinery QC
- Final Conclusion
Understanding Why Rigorous Quality Inspection Matters for Farm Equipment
Agricultural machinery operates under far harsher working conditions than most industrial tools. Constant soil abrasion, heavy cyclic loads, extreme temperature shifts, long continuous running hours and exposure to water, mud and corrosive fertilizers put every component under relentless stress. A small manufacturing defect discovered after shipment can lead to catastrophic operational losses: missed planting or harvesting windows, costly field downtime, expensive spare part replacements, and permanent damage to your regional brand reputation.
For global importers, distributors and bulk resellers, pre-shipment quality inspection is not an optional add-on—it is a risk-mitigation necessity. Unlike consumer goods, farm equipment failures directly impact your end customers’ income streams. Even minor oversights such as weak blade welding, untested hydraulic seals or missing safety guards can trigger warranty claims, customs hold-ups or even workplace injury liability lawsuits in EU, US and Australian markets.
This step-by-step guide is built exclusively for international procurement teams, independent importers and wholesale agricultural equipment buyers. It standardizes every inspection stage with measurable, repeatable criteria aligned with global ISO, CE and OSHA standards, eliminating ambiguous verbal agreements with manufacturers.
Core Pre-Inspection Preparation & Document Verification
Before physical machine inspection begins, complete a full audit of supporting paperwork to eliminate specification mismatches early. This phase filters out major order errors before you allocate time for on-site testing.
- Cross-reference purchase order against factory production drawings and final sample confirmation sheet Confirm all model numbers, engine power ratings, attachment configurations and color finishes match your signed contract. Many shipment disputes stem from unapproved factory design tweaks without buyer notification.
- Validate technical documentation set Complete user manuals (local language versions for your target market), spare parts catalogs, exploded assembly diagrams and maintenance schedules must be included for every unit ordered. Missing manuals will result in customs delays in most Western territories.
- Request original test reports Ask the supplier to provide factory batch test records covering engine performance, noise, vibration and leak testing. Cross-check serial numbers on test certificates against physical machine serial plates to avoid generic, non-specific lab reports.
- Prepare inspection reference tools Bring calipers, torque wrenches, noise meters, pressure gauges and AQL sampling sheets to standardize measurements during on-site QC. For bulk orders, follow international AQL 105 sampling standards for representative batch testing.
Step 1: Visual & Structural Full Machine Inspection
Visual inspection identifies manufacturing workmanship flaws that signal long-term durability risks. Complete this check before starting any engine or functional testing.
- Frame & Chassis: Scan all welding joints for incomplete penetration, cracks, pinholes or uneven bead work. Tap frame sections lightly to detect hollow, thin-gauge steel substitutions. Check paint and powder coating for peeling, bubbles, uneven coverage or bare metal exposure—poor coating leads to rapid rust in farm environments. Measure key frame dimensions to confirm compliance with drawing tolerances.
- Fastener Audit: Inspect all bolts, nuts and lock washers. Missing lock washers, loose hardware or mixed-grade fasteners are frequent factory shortcuts that cause assembly failure under vibration. All critical load-bearing bolts must be torqued to documented specifications.
- Serial & Marking Plates: Verify permanent metal serial plates are riveted securely to the main frame. Model, power, weight and safety warning labels must be printed in durable UV-resistant ink without fading or smudging. No hand-stamped, temporary stickers are acceptable for export units.
- Surface Defect Screening: Check for dents, bent sheet metal, plastic casing cracks and sharp exposed edges that create operator cut hazards. All sharp metal edges must be deburred during production.
Step 2: Critical Power & Engine System Functional Testing
The engine is the core asset of all agricultural machinery; incomplete power testing accounts for over 60% of post-delivery buyer complaints. Run every test under factory load conditions, not just idle state.
- Cold & Hot Start Test Perform three consecutive cold starts with standard-grade fuel. The engine must ignite within 3 pulls for handheld petrol units, or one key turn for larger machinery. No flooding, backfiring or persistent hard-start issues are permitted. After 30 minutes of continuous running, repeat hot start checks to identify heat-related fuel pump or carburetor faults.
- Idle & Full Load Performance Monitor idle speed stability for 5 full minutes—no surging, stalling or irregular RPM fluctuation. Apply rated operational load (attach cutting blades, tiller drums or pump heads) and run at maximum throttle. Listen for consistent, smooth combustion sound; rattling, knocking or high-pitched whines indicate internal piston, bearing or crankshaft defects.
- Emission & Smoke Inspection At idle and full load, exhaust must emit only thin, clear vapor. Thick black smoke signals carburetor over-fueling; blue smoke confirms internal oil leakage into combustion chambers, a fatal engine flaw that shortens service life drastically.
- Fluid Leakage Check After 30 minutes of running, wipe engine block, fuel tank lines, oil pan and exhaust manifolds. Any seepage of gasoline, engine oil or coolant counts as a major reject defect. Fuel hose clamps must be fully tightened with no soft plastic tubing exposed to hot exhaust components.
- Cooling System Validation Touch radiator, fan housing and cylinder head after sustained operation. Overheating (excessively hot casing without cooling airflow) points to blocked fins, faulty fans or undersized cooling systems designed to cut factory costs.
Step 3: Hydraulic, Transmission & Moving Assembly Inspection
Transmission and hydraulic failures create expensive field breakdowns, especially for tillers, tractors and spray rigs. Inspect all moving linkages under dynamic load.
- Gearbox & Drive Shafts: Shift all speed ranges multiple times; gear engagement must be smooth with no grinding or slipping. Check gearbox oil for metal particles by draining a small sample during inspection—silver flakes inside signal premature gear wear. PTO shafts must rotate evenly without wobble.
- Hydraulic Circuit Testing: Activate all hydraulic lift, spray and steering functions at maximum pressure. Check cylinder rods, rubber hoses and brass fittings for pinhole leaks, bulging hose walls or cracked plastic connectors. Pressure gauge readings must match the machine’s rated working pressure without sudden drops.
- Belt & Chain Drives: Inspect drive belts for fraying, uneven thickness or misaligned pulleys. Chains must be properly tensioned with full lubrication applied at the factory; rusted, dry chain assemblies are non-compliant for export shipments. All rotating drive points require rigid mounting brackets to eliminate excessive vibration.
- Vibration Measurement: Run equipment at full load and measure hand-arm vibration levels against ISO 22868 standards. Excessive vibration causes long-term operator discomfort and loosens internal fasteners during extended field use.
Step 4: Safety Component & Compliance Standard Check
Safety compliance is mandatory for cross-border sales; missing or damaged safety guards will result in customs seizure and market bans in the EU, USA and Canada. This inspection phase has zero tolerance for critical defects.
- Physical Safety Guards Every rotating blade, chain, belt, fan and exhaust component requires a rigid, impact-resistant protective shield. Guards cannot be easily removed without specialized tools. Partial, flimsy plastic covers that shift during operation are classified critical defects requiring full rework before shipment.
- Emergency Stop Controls All powered machinery must feature clearly labeled emergency shutoff switches within easy operator reach. Test E-stop functionality under full load—engine power must cut instantly with no delay. Handheld tools require spring-loaded throttle safety locks to prevent accidental acceleration.
- Warning & Instruction Decals Permanent, high-visibility warning labels must cover hazards including fuel flammability, cutting blade risk, hot exhaust surfaces and ear/eye protection requirements. All text must match your target market’s primary language. Faded, peeling or incomplete warning stickers fail compliance audits.
- Electrical Safety Check For battery-powered cordless tools and electric start engines: Inspect wiring insulation for cracks, exposed copper and loose terminal connections. All electrical circuits require fuse protection to avoid short-circuit fire risks. Switches must maintain consistent contact without intermittent power loss.
Step 5: Category-Specific Inspection Checklists
Handheld Garden & Forestry Tools (Chainsaws, Brush Cutters, Hedge Trimmers)
- Cutting attachment impact test: Blades and trimmer heads must withstand controlled impact without bending or cracking
- Harness & balance test: Backpack units must distribute weight evenly; loose shoulder straps create operator fatigue and safety risks
- Fuel tank integrity: Compress sealed tanks to detect pinhole leaks; tank caps must form an airtight seal to prevent spillage during transport
- Noise level testing: Meet ISO 22868 noise emission limits to comply with EU workplace noise regulations
Rotary Tillers, Cultivators & Soil Preparation Equipment
- Tiller blade torque test: All cutting tines must resist loosening under full soil load simulation
- Wheel steering responsiveness: Front/rear steering assemblies must turn without binding or delayed reaction
- Depth adjustment lock: Height positioning latches must stay fixed during heavy tilling, eliminating sudden depth shifts
- Mud sealing: Wheel hubs and axle joints require complete rubber dust seals to block soil intrusion into bearings
Sprayers, Water Pumps & Irrigation Machinery
- Tank pressure hold test: Pressurize plastic/metal tanks to rated working pressure and hold for 10 minutes; any pressure drop signals leakage
- Nozzle uniformity test: Run full water flow and confirm consistent spray pattern with no clogged or uneven output
- Pump diaphragm inspection: Check for thin, brittle rubber diaphragms prone to rupture under chemical fertilizer exposure
- Filter integrity: Inlet strainers must be fully seated to prevent sediment damage to internal pump components
Generators & Portable Power Units
- Voltage stability test: Measure AC output under 0%, 50% and 100% rated load; voltage fluctuations exceeding 5% damage connected farm electronics
- Ground wire installation: Mandatory earth grounding terminals with thick copper wire to eliminate electric shock hazards
- Outlet safety covers: All AC receptacles require childproof plastic shutters as required by US and EU electrical codes
- Fuel shutoff valve: Functional cutoff valve to stop fuel flow during transport and maintenance
Step 6: Component & Accessory Quality Validation
Global buyers frequently overlook loose accessories and replacement parts, which lead to incomplete shipments and customer dissatisfaction. Systematically cross-check every included item against your order bill of materials.
- Standard Attachments All ordered cutting blades, augers, spray wands, extension poles and wheel assemblies must be included in full quantity. Verify accessory material grade—low-carbon, thin replacement blades will dull after minimal field use.
- Spare Part Kits Confirm factory-supplied spare sets (spark plugs, air filters, fuel lines, replacement trimmer heads, gaskets) match your negotiated package contents. Missing spare kits increase your after-sales service overhead.
- Personal Protective Equipment (PPE) If PPE (safety goggles, anti-vibration gloves, ear defenders, leg guards) is included with machinery, inspect for tear resistance and certified impact protection labels. Thin disposable plastic safety gear fails Western market compliance rules.
- Fastener & Hardware Packs Small hardware bags with replacement bolts, lock nuts and washers must be sealed and labeled clearly to avoid loss during container transit.
Step 7: Packaging & Shipment Condition Inspection
Even fully functional machinery can arrive damaged due to inadequate factory packaging. Complete this inspection before container loading commences.
- Unit Protection: Every machine must be wrapped in scratch-resistant foam plastic; sharp metal corners require separate foam caps to puncture shipping cartons or wooden crates.
- Crate & Carton Strength: Export wooden crates must use solid plywood with reinforced corner bracing. Cardboard cartons for handheld tools need double-wall construction to resist stacking compression damage.
- Moisture Prevention: Desiccant silica gel packs must be placed inside all sealed packaging to stop rust formation during long ocean transit. Anti-rust oil coating is required for all exposed metal cutting components.
- Shipping Label Audit: Outer carton markings must clearly display model number, quantity, weight, country of origin and handling hazard symbols (flammable fuel, fragile, heavy lift). Illegible labels cause misrouting and customs sorting errors.
- Container Loading Supervision (Optional High-Value Add-On) For full container loads, assign an inspector to monitor loading to prevent improper stacking, heavy machinery crushing smaller units or loose shifting during sea transit.
Step 8: Defect Classification & Shipment Decision Rules
Classify all identified defects into three standardized tiers to create clear, enforceable agreements with manufacturers:
- Critical Defects – Shipment STOPPED, Full Rework Required Before Re-Inspection Missing safety guards, brake/pump total failure, severe oil/fuel leakage, cracked main frame, uncertified engine emissions, exposed live electrical wiring, non-functional emergency stop. Any single critical defect blocks shipment until fully repaired and re-tested.
- Major Defects – All Units With Defects Must Be Replaced Or Repaired Persistent engine smoke, gear slipping, hydraulic pressure loss, bent cutting components, unreadable safety labels, incorrect model specifications, broken packaging that risks transit damage. Batch shipment can only proceed after 100% rework and secondary inspection.
- Minor Defects – Negotiated Concession Allowed With Supplier Credit Minor cosmetic paint scratches, faint surface marks, loose non-structural plastic trim, slightly uneven decal placement. Minor defects do not impact machine performance or compliance, but buyers should negotiate partial order discounts to compensate for cosmetic downgrades.
Step 9: International Compliance Certifications Buyers Must Verify
Certification paperwork cannot be accepted solely via emailed PDF files; validate authenticity through official regulatory databases to avoid counterfeit documents that trigger customs confiscation.
- CE Mark (European Economic Area Mandatory) Confirm the Declaration of Conformity (DoC) lists the exact machinery model, relevant Machinery Directive 2006/42/EC and harmonized standards (EN ISO 4254, EN ISO 11806). Cross-check the notified body four-digit code via the EU NANDO database to confirm valid accreditation scope for agricultural equipment, not general consumer electronics.
- ISO 9001 Factory Quality System Verify the certificate belongs to the actual manufacturing plant producing your order, not a parent trading company without production facilities. Valid ISO certification proves consistent in-process QC across mass production batches.
- EPA Emissions (United States Import Rule) All petrol and diesel farm machinery requires EPA engine emission certification. Request engine serial number matching EPA test reports to avoid border detention.
- BSCI & Social Compliance For large retail distribution clients, BSCI factory audit reports confirm ethical labor standards, eliminating brand reputation risk from supply chain labor violations.
- RoHS & EMC Electromagnetic Compliance Machinery with electronic control boards must pass EN ISO 14982 EMC testing to prevent sensor interference in precision farming equipment. RoHS restricts hazardous heavy metals in wiring and circuit boards for EU markets.
Step 10: Advanced Lab & Field Performance Testing Techniques
For high-volume, long-term supplier partnerships, supplement factory visual inspection with third-party independent lab testing to validate long-term durability:
- Abrasion Wear Testing: Accelerated soil abrasion cycles on cutting blades to measure service life under continuous field use
- Salt Spray Corrosion Test: 500-hour salt chamber exposure to validate coating rust resistance in coastal, humid agricultural regions
- Continuous Endurance Run Test: 100-hour non-stop engine operation to detect premature bearing, gasket and fuel system failure
- Temperature Cycle Testing: Alternating hot/cold chamber cycles to test plastic component brittleness and seal contraction/expansion
- Field Trial Simulation: Recreate local soil, grass and crop conditions to measure real-world cutting, tilling and pumping efficiency
Frequently Asked Questions About Agri Machinery QC
Q1: How many units should I inspect for bulk container orders?
Follow international AQL 105 standard sampling. For agricultural equipment classified as high-risk machinery, use AQL 0.65 for critical safety defects and AQL 1.0 for major functional faults to ensure representative batch coverage.
Q2: Can I rely on the factory’s internal test reports alone?
Factory test records serve only as preliminary reference. Independent third-party inspection eliminates bias and factory testing shortcuts, providing legally defensible evidence for shipment dispute resolution.
Q3: What happens if a shipment arrives with hidden engine defects post customs clearance?
Without pre-shipment inspection records, manufacturers frequently reject warranty claims. Full QC documentation with serial number matching test results creates binding contractual leverage for repair, replacement or partial refunds.
Q4: Are handheld garden tools held to the same safety standards as large tractors?
Yes. EU and US safety regulations apply equally to all powered agricultural equipment, from small trimmers to heavy tillers. Missing blade guards or untested throttle locks trigger identical import penalties.
Q5: How long does a full pre-shipment inspection take per production batch?
A standard mixed batch inspection (power tools, tillers, sprayers) takes 4–6 hours for a 20-foot container load, including document audit, visual screening and full functional load testing of sampled units.
Final Conclusion
Comprehensive agricultural machinery quality inspection is the foundation of stable, profitable global procurement. This guide structures every inspection stage around measurable, market-aligned criteria to eliminate ambiguous quality agreements with manufacturers. By combining pre-production document audits, full structural and functional testing, safety compliance validation and packaging oversight, international buyers can drastically reduce post-shipment warranty costs, customs risks and end-customer churn.
Prioritize critical safety and power system testing above cosmetic checks—field operational reliability is what determines long-term success for your agricultural equipment distribution business. Always retain fully signed, serial-number matched inspection reports as contractual protection for all bulk wholesale orders.